Streetwear brands lose money on prints for one reason: they pick the method before they know their volume. A 2-colour logo that costs €0.90 screen-printed at 500 units costs €4.20 DTG-printed at the same volume in our quoting data from Portuguese factories. Multiply that across a 2,000-unit drop and the print choice alone shifts margin by €6,600. The "best" method isn't universal. It changes with unit count, design complexity, fabric blend, and the wash life the buyer expects.
This guide compares screen printing, DTG, DTF (direct-to-film), and sublimation the way a production manager compares them: at fixed volumes, on specific fabrics, against measurable wash and lightfastness standards. The numbers come from real job sheets across the Porto-region factory pool we work with, not vendor marketing.
Heads up: We're Portugal Clothing Factory, a group of 80 documented Portuguese clothing factories. The cost ranges below come from quotes across Portuguese print and cut-and-sew factories between 2024 and 2026. EUR throughout, manufacturer-group lens.
Key Takeaways
- Screen printing wins on cost above roughly 100-150 units; per-unit prices drop to €0.55-€1.10 at 1,000+ units for 2-colour jobs
- DTG makes sense for runs under 50 units and for photographic or high-colour-count artwork
- DTF (direct-to-film) is the new mid-volume sweet spot for complex multi-colour designs from 30 to 200 units
- Sublimation only works on polyester-heavy fabrics (minimum 65% poly) and light base colours
- Portuguese factories typically set up for screen-printing efficiency at 300+ units; below that, DTG, DTF, or transfers are faster and cheaper
- Most print failures trace to the artwork file rather than the press, and almost all of them are caught by a signed pull-down before the run
- Embroidery, the largest decoration category at about 29% of 2025 decorated-apparel revenue, costs more than every print method and is chosen for perceived value and for caps
- Mixing methods across a single drop is normal and often the right answer
Try it free: Pressure-test these numbers for your specific product with our garment cost calculator. 60 seconds, no email required.
What Is Screen Printing?
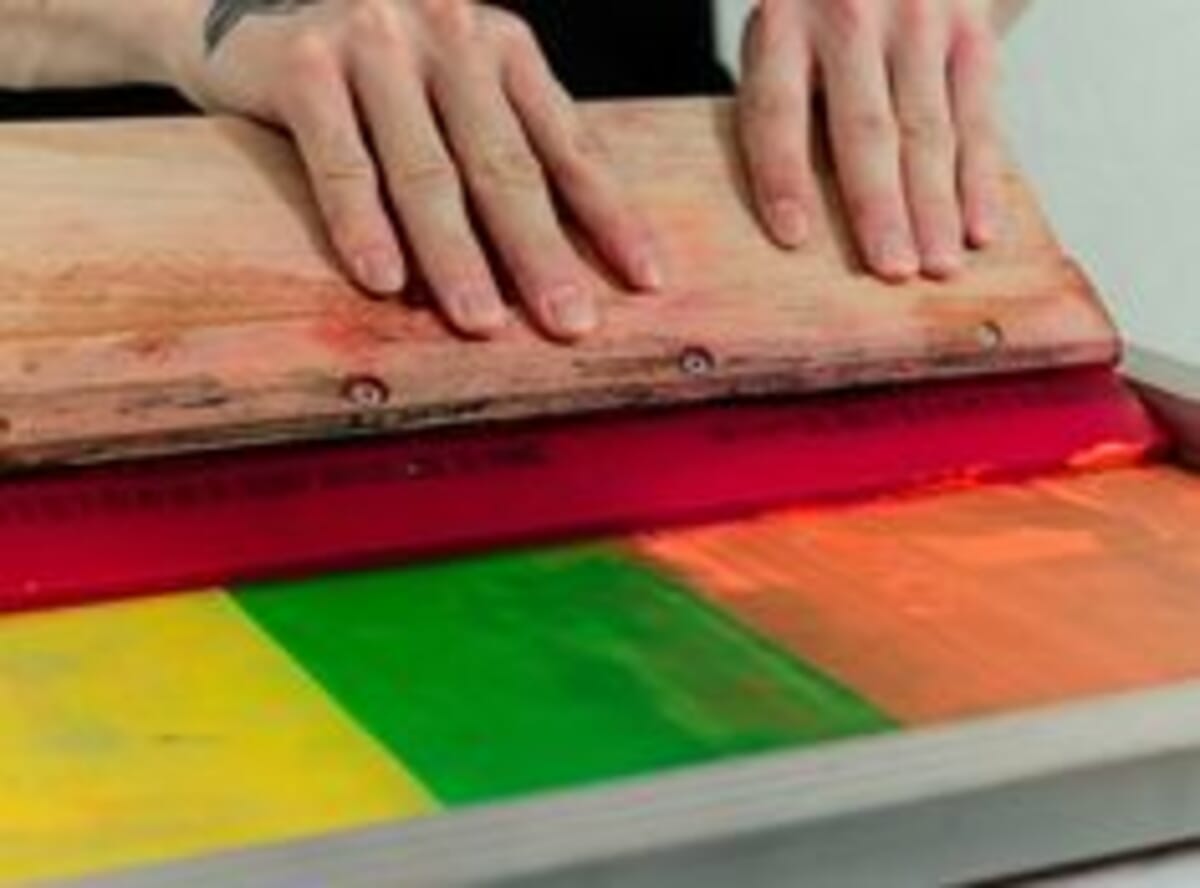
Screen printing pushes ink through a mesh stencil onto fabric, one colour per screen. The method dominates streetwear manufacturing above 100 units because the per-unit ink and labour cost collapses once screens are set up. Screen printing took about 26% of the US$37.6 billion decorated apparel market in 2025, second to embroidery at 29% and ahead of digital printing at 21% (Fortune Business Insights, 2025). Note those are revenue shares: screen printing is cheaper per unit than the others, so its share of actual garments decorated is higher than 26%. An earlier version of this article claimed 60% of global decoration volume, which no published source supports.
How the screen printing process works
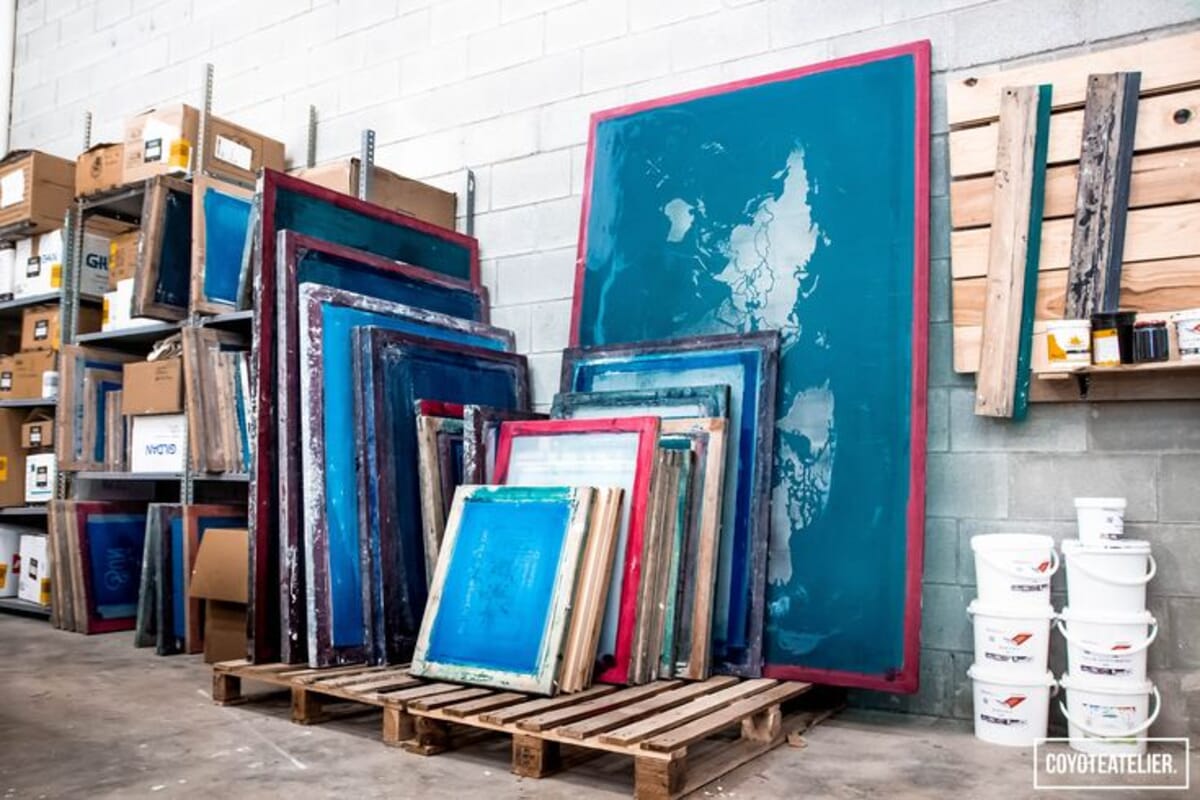
A separator breaks the artwork into individual colour layers. Each layer gets burned onto a mesh screen. The screens load onto a rotary press, and ink is pulled across each screen with a squeegee, one colour at a time. The garment then passes through a flash dryer at 160-170°C to cure the plastisol or water-based ink.
Strengths
Screen printing hits the lowest cost per unit at volume. It prints bright, opaque colours on dark fabrics, handles specialty inks (puff, high-density, discharge, metallic, glitter, glow-in-the-dark), and holds colour through the equivalent of 50 or more home launderings when cured correctly, which is about ten AATCC TM61 cycles. Specialty inks alone make it the only viable route for certain streetwear aesthetics (puff print, metallic finishes, discharge "vintage washed" looks).
Weaknesses
Setup cost is fixed per colour. A 6-colour front graphic carries roughly €300-€500 in screen and separation fees before the first shirt prints, at the €30-€80 per screen our factories quote. It's uneconomic under 50 units, and fine gradients require halftone tricks that look grainy on heavy cotton. Screens take physical storage space, which means reorders 18+ months later sometimes require re-burning.
Citation Capsule: Screen printing held about 26% of the US$37.6 billion decorated apparel market in 2025, behind embroidery at 29% (Fortune Business Insights, 2025), and its unit economics come from amortising fixed screen setup. On PCF quoting records a 2-colour plastisol placement in Portugal runs about €0.90 at 500 units and €0.70 at 1,000, against a fixed setup near €156 for the two screens.
What Is DTG (Direct-to-Garment) Printing?
DTG sprays water-based pigment ink directly onto the garment, the same way an inkjet printer handles paper. It's built for low volumes and complex artwork. Setup is zero and any design prints for the same price as any other, which is why it dominates the sub-25-unit tier. Digital printing as a whole held about 21% of 2025 decorated-apparel revenue and is the fastest-growing decoration category (Fortune Business Insights, 2025). We have dropped a previously quoted figure putting 80%+ of sub-25-unit orders on DTG, because we could not find a published source for it.
How DTG works
The garment is pretreated with a bonding solution, loaded onto a platen, and the printer deposits CMYK and white ink layers guided by an RGB or CMYK file. A heat press cures the ink at about 165°C for 90 seconds. No screens, no separations, no colour-by-colour setup.
Strengths
DTG handles photographic images, gradients, and unlimited colour counts at the same price. It's economical from 1 unit up to roughly 50-100 units. Hand-feel is soft on cotton, since the ink penetrates rather than sitting on top.
Weaknesses
Print speed is 60-90 seconds per shirt versus 4-6 seconds on an automatic screen press. Ink cost is 3-5x higher per unit. White ink on dark garments fades faster, losing visible density after 20-25 washes in third-party testing. DTG also struggles on anything under 80% cotton. In our placement records, DTG jobs over 200 units block Portuguese factory production lines for a full day, which is why factories quote them at a premium above that volume or push clients toward screen printing with simplified artwork.
What Is DTF (Direct-to-Film) Printing?
DTF is the method most streetwear guides still ignore in 2027, even though it's reshaping the mid-volume tier. DTF prints the design onto a special PET film, applies a hot-melt adhesive powder, then heat-presses the film onto the garment. The result has the colour vibrancy of DTG with the wash durability of screen printing and works on virtually any fabric, including polyester, cotton blends, and nylon.
Strengths
DTF works across cotton, polyester, blends, and synthetics. Wash durability typically 30-40 cycles before visible degradation, better than DTG. No setup cost, so multi-colour designs print at the same per-unit cost. Sweet spot is 30 to 200 units for complex multi-colour designs that would be punitive on screen printing setup costs.
Weaknesses
Hand-feel is rubbery rather than soft, similar to a heat transfer. Visible film edge on close inspection. Less suitable for premium positioning where buyers expect screen-printed or water-based-print hand-feel. White is not as opaque as plastisol on dark fabrics, though improving with newer DTF systems.
DTF is the method we recommend when brands they have 80-150 unit runs of multi-colour designs. A 6-colour graphic carries roughly €376 of screen setup before the first shirt prints, which is €2.50-€4.70 per unit at those volumes and more than the entire DTF price. The trade-off is the slightly synthetic hand-feel.
What Is Sublimation Printing?
Sublimation uses heat to turn solid dye into gas that bonds with polyester fibres, producing prints that cannot crack, peel, or fade on the fabric surface. It is the smallest of the four print methods in streetwear, because most streetwear is cotton or cotton-heavy. Across decorated apparel generally dye sublimation is not small at all, at roughly 18% of 2025 revenue (Fortune Business Insights, 2025), but that share sits in sportswear and polyester activewear rather than cotton streetwear. An earlier version of this article put it under 8% of European decoration, a figure we cannot source.
How sublimation works
Artwork prints onto transfer paper with sublimation ink. The paper is pressed against a white or light polyester garment at 190-200°C for 45-60 seconds. The dye vaporises and permanently dyes the fibres. There's no ink layer, so the print is weightless.
Strengths
Unlimited colours, no hand-feel, full-coverage all-over prints, and durability tied to the fabric itself. It's the only viable method for all-over-print hoodies, jerseys, and technical streetwear pieces in polyester.
Weaknesses
Sublimation only works on polyester (minimum 65%, ideally 100%) and only on white or very light base fabrics. It cannot print on cotton, which rules out most classic streetwear hoodies and tees. White seams and creases show through as "ghosting" on all-over prints. Most brands that ask us about sublimation actually want DTG, DTF, or cut-and-sew from pre-printed fabric. They've seen an all-over-print hoodie online and assumed it was a universal option. On the 300 GSM cotton fleece that defines premium streetwear, sublimation is physically impossible.
How Does Embroidery Compare on Cost and Durability?
Embroidery is the decoration method this comparison used to skip, and it should not have: it is the largest decoration category in the market. In the 2025 decorated apparel market, embroidery took about 29% of revenue against screen printing's 26%, digital printing's 21% and dye sublimation's 18% (Fortune Business Insights, 2025).
Embroidery stitches thread through the fabric rather than laying ink on it, so it is a different kind of decision from the four print methods. It cannot reproduce a photograph, a gradient or a large multi-colour graphic. What it can do is signal quality at close range, which is why it owns caps, chest logos and structured outerwear.
When embroidery beats printing on cost
Almost never on a like-for-like graphic, and that is the point. A chest logo runs €2.50-€7 per unit plus a one-time €50-€200 digitising fee, which lands it near DTG and above screen printing at every volume in the table above. Cost is not the reason to choose it.
The reason is perceived value. A stitched chest logo reads as more expensive than a printed one at the same retail price, and above roughly €100 retail buyers increasingly expect it. On caps it is effectively the only option, because curvature and panel seams defeat both DTG and sublimation.
What drives the embroidery price
Stitch count, not area. Factories quote per thousand stitches, so a dense fill costs several times a line-art mark of the same size. A simple wordmark might be 4,000 stitches; a detailed crest 15,000 or more. Reducing stitch density is the single biggest lever on an embroidery quote.
| Placement | Typical stitch count | Cost per unit | Digitising (one-time) |
|---|---|---|---|
| Small wordmark or line-art logo | 3,000-6,000 | €2.50-€4 | €50-€100 |
| Standard chest logo | 6,000-10,000 | €3-€7 | €50-€200 |
| Large back or sleeve piece | 15,000-40,000 | €6-€18 | €100-€400 |
| Cap front (structured) | 5,000-12,000 | €2.50-€6 | €50-€200 |
PCF aggregated embroidery-vendor quotes 2024-2026 across Porto and Braga. Digitising is charged once per design and reused on reorders, so ask the vendor to release the stitch file.
How long does embroidery last?
Longer than any print, with a different failure mode. Thread does not crack or peel, so there is no wash ceiling in the sense that applies to plastisol or DTG. What fails instead is the backing and the fabric around the stitches: puckering on light jersey, and thread snags on loose knits. Embroidery on 140 GSM jersey is a common and avoidable mistake, because the fabric cannot carry the stitch tension. Specify a cut-away backing on anything under 200 GSM.
Citation Capsule: Embroidery is the largest apparel decoration category at roughly 29% of 2025 decorated-apparel revenue, ahead of screen printing at 26%, digital printing at 21% and dye sublimation at 18% (Fortune Business Insights, 2025). A chest logo costs €2.50-€7 per unit plus €50-€200 digitising, so it is dearer than screen printing at every volume. It is chosen for perceived value and for caps, not for cost, and it is priced per thousand stitches rather than by area.
What's the Cost Per Unit at Real Production Volumes?
Print method economics hinge on one variable: setup cost amortised across units. Below is real per-unit pricing from Portuguese cut-and-sew and print factories for a 2-colour front graphic on a mid-weight cotton tee, in EUR, excluding the blank garment. Multi-colour and back prints scale roughly linearly with colour count.
| Units | Screen printing | DTG | DTF | Sublimation (poly blanks) | Embroidery (chest logo) |
|---|---|---|---|---|---|
| 50 | €3.80 | €3.20 | €3.40 | €4.10 | €5.80 |
| 100 | €2.10 | €3.10 | €2.80 | €3.90 | €4.40 |
| 300 | €1.10 | €3.00 | €2.50 | €3.60 | €3.30 |
| 500 | €0.90 | €2.95 | €2.40 | €3.40 | €3.05 |
| 1,000 | €0.70 | €2.90 | €2.30 | €3.20 | €2.80 |
| 5,000 | €0.55 | €2.85 | €2.20 | €2.90 | €2.60 |
PCF print-vendor and factory job sheets, March 2024 to February 2026, averaged across Porto-region factories. Print columns are a 2-colour plastisol front graphic on a 180 GSM cotton tee, excluding the blank garment. The embroidery column is a single chest logo of roughly 8,000 stitches including the €50-€200 digitising fee amortised over the run, and is not directly comparable to the print columns: embroidery cannot reproduce a large multi-colour graphic at all. Sublimation assumes polyester blanks, which themselves cost €1-€2 more than mid-weight cotton.
How to read this table
Screen printing breaks even against DTG at about 62 units on a 2-colour design, and the crossover moves sharply right as colours stack up, as the next section works out. Above 300 units a 2-colour screen job is 2-3x cheaper than DTG. DTF sits between DTG and screen printing across most volume tiers and wins outright on 4+ colour designs in the 50-200 unit window. Sublimation's flat curve looks competitive at 5,000 units but ignores that the polyester blank itself costs €1-€2 more than mid-weight cotton.How much does each extra colour cost?
The table above is 2-colour. Every additional screen adds €30-€80 of setup plus €0.20-€0.50 of ink and labour per unit. Both halves matter, and guides routinely quote only the second one, which is how brands end up with a quote twice what they budgeted.
Fit a setup-plus-variable curve to our own 2-colour figures above and it resolves to roughly €156 of setup and €0.54 per unit. That model reproduces every row in the table to within four cents, so we can use it to work out where screen printing stops being the cheap option as colours stack up.
| Colours in the design | Screen setup | Screen cost per unit (variable) | Break-even against DTG |
|---|---|---|---|
| 2 | €156 | €0.54 | 62 units |
| 3 | €211 | €0.89 | 98 units |
| 4 | €266 | €1.24 | 147 units |
| 6 | €376 | €1.94 | 340 units |
| 8 | €486 | €2.64 | about 1,200 units |
Computed from the per-unit table above, using €55 of setup and €0.35 of ink and labour per additional screen (the midpoints of the ranges in this section) against a flat DTG price of €3.05 at these volumes. Your factory's screen fee moves the break-even, so substitute its number.
The break-even climbs faster than most brands expect. On a 2-colour graphic screen printing is cheaper from about 62 units. On a 6-colour graphic it needs about 340. By 8 colours the per-unit ink and labour alone nearly equals DTG's flat price, so the break-even runs past a thousand units.
A worked correction on six colours
An earlier version of this article put a 6-colour design at 200 units at €2.50 per unit on screen printing against €3.00 on DTG, and concluded screen printing still won. That calculation used the 300-unit price for a 200-unit run and left out the four extra screens entirely. Done properly, a 6-colour job at 200 units costs €2.72 to €4.92 screen-printed, around €3.82 at the midpoints, against €3.05 on DTG and about €2.65 on DTF. At six colours and 200 units DTF is the cheapest of the three and screen printing is most likely the dearest.
The Portuguese production context
Portuguese factories concentrate in the Minho region and operate high-capacity automatic screen presses optimised for 300-5,000 unit runs. DTG stations exist but are usually outsourced or run as a secondary service. DTF capacity has grown sharply since 2023 and is now widely available across Porto and Braga. This means minimum order quantities for screen printing in Portugal typically start at 100-150 pieces per design, while DTG and DTF have no MOQ but DTG carries a 15-20% price premium versus larger DTG-focused countries.
Citation Capsule: Screen printing's per-unit cost drops sharply with volume due to setup-amortization, becoming cheapest at 200+ unit runs with 1-4 colors. DTG holds steady regardless of volume, making it cost-effective for limited drops and high-color complexity. DTF sits between, and sublimation requires polyester or poly-blend fabrics.
How Do Quality and Durability Compare?
Wash durability is where cheap print jobs expose themselves, and it is also where the terminology gets abused. AATCC TM61 is a colourfastness test, not a wash counter. One 45-minute cycle of Method 2A approximates five home launderings, and the result is a 1-to-5 grey-scale grade for colour change, not a number of washes.
So the two things get reported together and should not be confused. The TM61 grade tells you how much colour shifted; the home-wash figures below are the practical equivalent our factories and their buyers work to, where 50 launderings is roughly ten TM61 cycles. An earlier version of this article stated that TM61 simulates 50 washes in 45 minutes, which overstated the standard tenfold.
| Method | Home-wash equivalent | TM61 colour grade | Colour accuracy | Hand-feel | Best fabric |
|---|---|---|---|---|---|
| Plastisol screen | 50+ launderings | 4-5 / 5 | Pantone match Δ-E 2-3 | Visible texture | Cotton, blends, denim |
| Water-based screen | 50+ launderings | 4-5 / 5 | Pantone match Δ-E 2-3 | Soft, sinks into fabric | Cotton |
| Discharge screen | 50+ launderings | 4-5 / 5 | Limited (chemical reaction) | Very soft, vintage | 100% cotton only |
| DTG | 20-25 launderings | 3-4 / 5 | CMYK only, no Pantone | Soft on cotton | 80%+ cotton |
| DTF | 30-40 launderings | 4-5 / 5 | CMYK + spot accent | Rubbery, visible film | All fabrics |
| Sublimation | Life of the fibre | 5 / 5 | CMYK | Zero hand-feel | 65%+ polyester, light only |
Home-laundering figures are the working numbers our factories and their buyers use, not a published standard. TM61 grades are the colour-change band those factories report on a 1-to-5 grey scale. Colour accuracy, hand-feel and fabric compatibility are production characteristics of each method rather than measured data.
Colour accuracy
Screen printing matches Pantone spot colours within a Delta-E of 2-3 when ink is mixed to standard. DTG works in CMYK and cannot hit true Pantone colours, especially bright oranges, greens, and fluorescents. DTF can approach Pantone with white-ink boost layers but isn't true spot-colour. Brands chasing tight colour standards pick screen printing for this reason alone.
Fabric compatibility
Screen printing works on cotton, cotton-poly blends, fleece, denim, and canvas. DTG needs 80%+ cotton to bond cleanly. DTF works on virtually any fabric. Sublimation requires 65%+ polyester. A production tech pack should specify both the fabric composition and the chosen print method, since a mismatch forces a reprint at the factory's cost or the brand's.
Hand-feel
Plastisol screen printing sits on top of the fabric with noticeable texture. Water-based and discharge screen inks sink into the fabric and feel soft. DTG feels soft on cotton. DTF feels slightly rubbery, similar to a vinyl transfer. Sublimation has zero hand-feel. Premium streetwear increasingly specifies water-based discharge prints to match the "worn-in" aesthetic, which is one reason discharge has held its premium positioning even as DTF has eaten into mid-volume screen printing.
Citation Capsule: Measured as home launderings before visible degradation, a correctly cured screen print holds through 50 or more, DTF through 30 to 40, and DTG fades visibly at 20 to 25, with white ink on dark garments going first. Sublimation lasts the life of the polyester fibre because it dyes the fibre rather than sitting on it. Under AATCC TM61 one 45-minute cycle approximates five launderings, so a 50-wash claim is about ten cycles.
Which Method Fits Which Streetwear Product?
The right method changes with product silhouette, fabric weight, and design type. In our own quoting records, hoodie orders above 200 units go to screen printing far more often than not, and sub-50 unit tee drops go to DTG almost by default. We have removed the precise percentages an earlier version of this article attached to those patterns, along with a Business of Fashion citation that did not support them.
Hoodies and heavyweight fleece (300+ GSM)
Screen printing is the default. Heavy fleece absorbs DTG ink unevenly, and sublimation is out because fleece is cotton-heavy. For photographic chest prints on hoodies, water-based screen printing with a halftone separation is the production standard. DTF works on hoodies for one-off custom orders but the rubbery hand-feel hurts premium positioning.
T-shirts (140-220 GSM cotton)
Under 50 units: DTG. From 50-200 units, DTF for multi-colour designs, screen for 1-3 colour. Above 300 units: screen printing almost always wins. Above 1,000 units: screen with 6+ colours becomes punitive on setup; consider simplifying the design.
Outerwear and jackets (nylon, polyester shells)
Screen printing requires adhesion-promoting inks. DTF works directly. Sublimation requires polyester base. Most streetwear outerwear uses embroidery, patches, heat transfers, or specialty DTF for printed graphics on shell fabrics.
Caps and headwear
Embroidery dominates. Screen printing appears on unstructured flat-brims; DTG and sublimation are rare on caps due to curvature and fabric. DTF works on the flat front panel of structured caps.
Design-type matchups
| Design type | Best method |
|---|---|
| Bold 1-3 colour graphic on cotton | Screen printing |
| Photographic / painted artwork | DTG (cotton) or DTF (any fabric) |
| Gradients | DTG, DTF, or halftone screen |
| 4-6 colour complex graphic, 50-200 units | DTF |
| 4-6 colour complex graphic, 300+ units | Screen printing (halftones if needed) |
| All-over patterns on polyester | Sublimation |
| All-over patterns on cotton | Cut-and-sew from pre-printed fabric |
| Puff print streetwear effect | Plastisol screen with puff additive |
| "Worn-in" vintage look | Water-based discharge screen |
| Reflective, glow, metallic, glitter | Specialty plastisol screen |
| Chest logo on a premium piece, or any cap | Embroidery |
| Small logo, under 50 units, cost is the priority | DTG or heat transfer vinyl |
Method-to-design matching from PCF print-vendor quoting and the briefs we handle, 2024-2026. This is a placement heuristic, not a ranking: a factory with unusual capability or a brand with an unusual hand-feel requirement will reasonably land elsewhere.
What Mistakes Ruin Prints in Production?
Most print failures trace to the artwork file rather than the press, and the fix is almost always free if caught before setup. We do not run presses, so we cannot put a percentage on it and have withdrawn the 70% figure an earlier version of this article quoted. What we see in briefs is a consistent shortlist: wrong resolution, missing colour separations, the wrong colour mode, and artwork built for a different method than the one quoted.
File-level mistakes
Incorrect colour separations. Screen printing needs vector artwork with each colour on its own layer. Sending a flat JPEG forces the factory to re-trace the design, which adds €80-€150 and introduces colour drift.
Low-resolution source files. DTG and DTF print at 1200 DPI. Artwork supplied at 72 DPI (typical for screen exports) comes out pixelated. Minimum is 300 DPI at print size.
RGB instead of CMYK or Pantone. Screen printing needs Pantone TCX/TPG references. DTG and DTF work in CMYK but render RGB greens, oranges, and fluorescents poorly. Convert before sending.
Artwork sized for the wrong placement. A chest logo file at 30 cm wide will print at 30 cm wide. Specify the print dimensions in your tech pack, separate from the artwork file size.
Missing pull-down sheets. A pull-down is a test print on the actual production fabric, approved by the brand before the full run. Skipping it is how brands end up with 1,000 hoodies printed in the wrong shade of orange. Every production job over 100 units should require a signed pull-down.
Production-level mistakes
Wrong ink for the fabric. Plastisol on nylon jackets peels within 5 washes. Water-based ink on 100% polyester tees washes out immediately. The tech pack must match ink chemistry to fabric composition.
Skipping cure verification. Improperly cured plastisol washes off in the first home laundry cycle. Ask the factory for a wash-test sample before bulk approval.
Mixing methods within a drop without QC plan. Brands that run screen-printed tees and DTG hoodies in the same drop often see colour mismatch between identical artwork on different products. If colour consistency matters, lock the method.
Ignoring under-base whites on dark fabrics. Printing colour ink directly on a dark hoodie without a white under-base produces muddy, low-saturation results. Specify under-base in your tech pack.
Citation Capsule: Print reprints trace to the artwork file far more often than to the press. The recurring faults are 72-DPI screen-exported artwork sent for DTG or DTF jobs that need 300 DPI at print size, flat raster files sent for screen printing that needs vector separations, and RGB colour references where Pantone or CMYK is required. A signed pull-down on the production fabric catches all three before the run.
What Should You Check Before Sending Artwork?
Before you send artwork to a Portuguese print vendor, audit the file against this list:
File format
- [ ] Vector (.AI,.EPS,.PDF) for screen printing
- [ ] 300 DPI minimum at print size for DTG, DTF, sublimation
- [ ] Each colour on its own layer for screen printing
- [ ] All fonts converted to outlines
Colour
- [ ] Pantone TCX or TPG references for screen printing colours
- [ ] CMYK colour mode for DTG and DTF
- [ ] No RGB as primary reference
- [ ] Under-base white specified for colour prints on dark garments
Sizing
- [ ] Print dimensions specified separately from file size
- [ ] Artwork at 1:1 scale for print size
- [ ] Bleed area defined for full-bleed prints
Method-specific
- [ ] Halftone screen settings specified (LPI) for screen halftones
- [ ] Discharge ink call-out for water-based discharge jobs
- [ ] Specialty effects (puff, glitter, reflective) flagged
- [ ] White ink layer separated for DTG on dark garments
Approvals
- [ ] Pull-down sheet requested before bulk
- [ ] Wash test sample requested before bulk
- [ ] Production placement diagram included in tech pack
If 80%+ of these checkboxes are filled, your artwork is print-ready.
How Does the August Shutdown Affect Print Timelines?
Most Portuguese factories close for 2 to 3 weeks in mid-August for the traditional summer break. Print vendors typically follow the same schedule. If your timeline crosses early-to-mid August:
- Submit artwork and approve pull-downs by mid-July
- Bulk print orders running through August often shift to September
- Plan around it for autumn drops; an August timeline shift can cost a launch window
Brands new to Portuguese sourcing get hit twice: once trying to start production in August, once trying to ship in late August. Build August out of your timeline from day one.
Running into production issues? Get in contact and tell us what you're making. We're a group of Portuguese factories and we answer every serious brief within 24 hours.
Frequently Asked Questions
What brands ask once they have the cost table: where DTG actually beats screen printing, how long each method really lasts in the wash, what the Portuguese minimums are, whether sublimation works on black, and when embroidery is the better call.
Is DTG ever cheaper than screen printing?
Yes. On a 2-colour design DTG is cheaper below about 62 units; on a 4-colour design below about 147; on a 6-colour design below about 340. DTG carries no setup cost, so it wins whenever the screen fees (€30-€80 each) cannot be spread across enough units. For photographic artwork DTG or DTF wins at any volume, because screen printing cannot reproduce it without halftones.
How long does screen printing last compared to DTG?
Properly cured plastisol screen prints hold colour through 50 or more home launderings, about ten AATCC TM61 cycles, with minimal loss. DTG prints typically show visible density loss after 20-25 washes, particularly white ink on dark garments. Water-based screen prints match or exceed DTG in softness and match plastisol in durability. DTF sits between, around 30-40 cycles.
Can you DTG on a hoodie?
Yes, on hoodies with 80%+ cotton face fabric and weights up to around 320 GSM. Heavier fleece absorbs ink unevenly and produces muted results. Most Portuguese factories push hoodie orders above 100 units to screen printing for consistency.
What's the minimum order for screen printing in Portugal?
Typical MOQ is 100-150 pieces per design, per colour. Some factories accept 50 pieces with a surcharge. Below 50 units, DTG, DTF, or heat transfers are almost always more economical, since screen setup costs dominate the per-unit price.
Does sublimation work on black hoodies?
No. Sublimation dye is transparent and only shows on white or very light polyester fabrics. Printing on black or dark garments with sublimation produces no visible image. Dark all-over-print looks require cut-and-sew from pre-printed polyester fabric or specialty discharge screen printing on cotton.
Should I use plastisol or water-based screen ink?
Plastisol for bright colours on dark fabrics, specialty effects, and lowest cost. Water-based or discharge for soft hand-feel, vintage aesthetic, and premium price points. Water-based ink costs 15-25% more per unit and requires tighter curing control, but matches the "broken-in" look buyers increasingly expect in premium streetwear.
When should I use DTF over DTG?
When you need wash durability above 25 cycles, when your fabric isn't 80%+ cotton, or when your volumes sit between 30 and 200 units with 4+ colours. DTF is the mid-volume sweet spot most brands underestimate. The trade-off is the rubbery hand-feel that hurts premium positioning above €120 retail.
What about embroidery instead of printing?
Embroidery is the right choice for chest logos, premium positioning, caps, and structured outerwear. Per-unit cost runs €2.50-€7 for a chest logo, plus €50-€200 digitising fee one-time. Embroidery typically signals higher quality than print at retail price points above €100 and is the standard for cap branding.
How many sample rounds should I expect on prints?
For first-run production: 1 pull-down sheet, then 1 production sample. For complex multi-colour or specialty effects: add 1 round. Most disputes happen when brands skip the pull-down to save the €30-€80 fee. Don't skip it.
Can I mix methods in a single drop?
Yes, and most professional drops do. A typical streetwear capsule might run screen-printed tees, DTF on a few experimental colourways, embroidery on caps, and sublimation on a polyester all-over-print piece. Plan the colour matching across methods carefully, since CMYK DTG and DTF won't match Pantone screen prints exactly.
How Should You Pick the Method Before a Drop?
Print method is a production decision, not a design decision. Pick it after you know the volume, the fabric, and the wash life the buyer expects.
- Screen printing earns its spot above 100-150 units, especially on 1-3 colour designs
- DTG owns the sub-50 range and photographic work on cotton
- DTF owns the 30-200 unit window for complex multi-colour designs across any fabric
- Sublimation solves specific all-over-print needs on polyester pieces
- Embroidery is the answer for caps and for chest logos on anything above roughly €100 retail, at a cost premium over every print method
Mixing methods across a collection is normal. A drop might run screen-printed tees, a DTF capsule with complex artwork, embroidery on caps, and a sublimated all-over jersey piece.
Brands that lose money on prints usually committed to the method before pricing the alternatives, sent artwork files built for the wrong process, or skipped the pull-down approval. All three are avoidable with a production-aware tech pack and a factory or specialist sourcing partner willing to flag mismatches before the press fires.
We're a group of 80 documented Portuguese clothing factories based in Porto and Guimarães. Tell us your product, volume, and timeline. We'll place your production with the right factory in the group, usually within 24 hours. You work directly with the factory. No commissions, no pitch, no upsell.
Get in contact Download the directory (€39)Need a tech pack? Get a factory-ready single-style tech pack for €79. See what's included.
Sources
- Fortune Business Insights, Decorated Apparel Market (2025). Source for the market size of US$37.6 billion and the decoration-type split: embroidery about 29%, screen printing 26%, digital printing 21%, dye sublimation 18%, other methods 6%. These are revenue shares, not unit volumes.
- AATCC TM61, Colorfastness to Laundering: Accelerated. Source for the test method only. One 45-minute cycle of Method 2A approximates five home launderings and produces a 1-to-5 grey-scale colour-change grade. AATCC does not publish wash-durability figures by decoration method, so the home-laundering figures in this article are our factories' working numbers, not a standard.
- PCF print-vendor and factory job sheets, March 2024 to February 2026, across the Porto-region print and cut-and-sew factories in our group. Source for every price in EUR on this page, the MOQ thresholds, and the embroidery stitch-count bands.
- The break-even table by colour count is computed from our own per-unit figures in this article, not taken from a source. The workings are shown so you can substitute your factory's screen fee.
- Earlier versions of this article cited CITEVE for Portuguese production data, EURATEX for European decoration statistics, Business of Fashion for streetwear decoration splits, Impressions Magazine for reprint causes and Printwear & Promotion for decoration market share. None of those organisations publishes the figures that were attributed to them, and those figures have been removed rather than re-sourced.
Related reading
- How to build a capsule collection
- Clothing manufacturing costs in Portugal
- Small batch clothing production in Portugal
- Red flags when picking a manufacturer
- How to start a clothing brand in Portugal
- MOQ minimums in Portugal
- How to order a clothing sample
- How to find a clothing manufacturer
- Quality control in Portuguese clothing production
Written by João Oliveira, Founder at Portugal Clothing Factory.